
 English
 中文简体
 Deutsch
 عربى
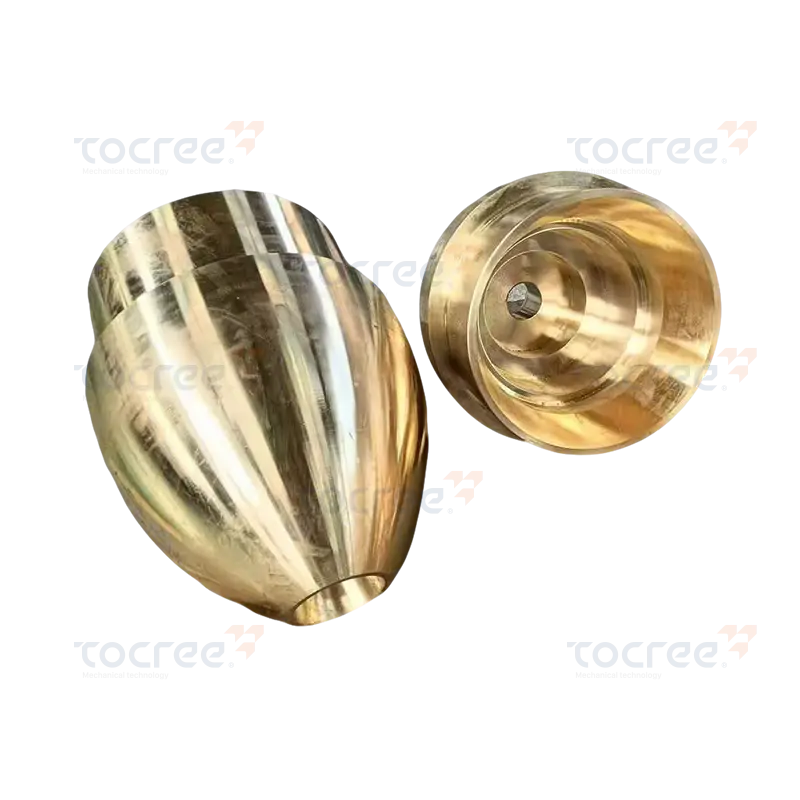
This straight sleeve is made of aluminum bronze alloy as the base material. According to c...
Products
-
-
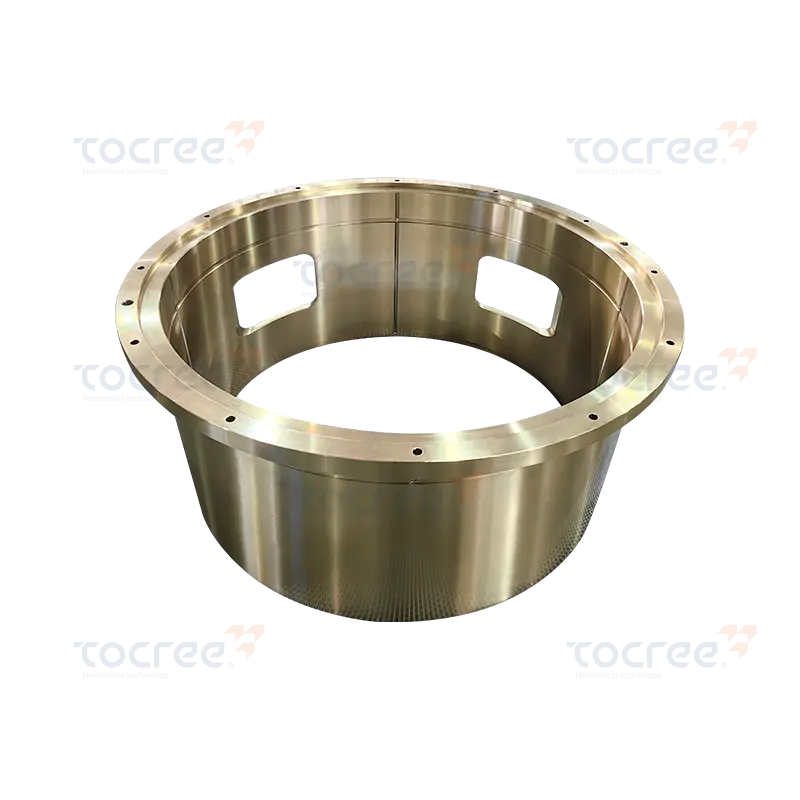 Singe Flanged Brass Bushing
The single-sided flange copper sleeve is a high-performance brass alloy shaft sleeve with ...
-
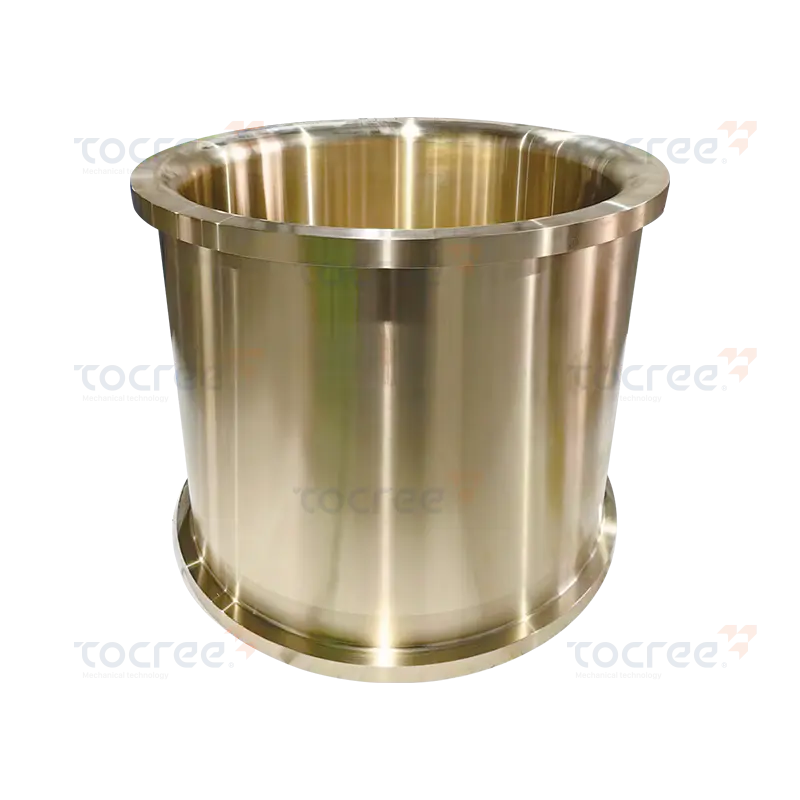 Double Flanged Brass Bushing
The double-flange brass bushing is a high-performance metal bushing, widely used in mechan...
-
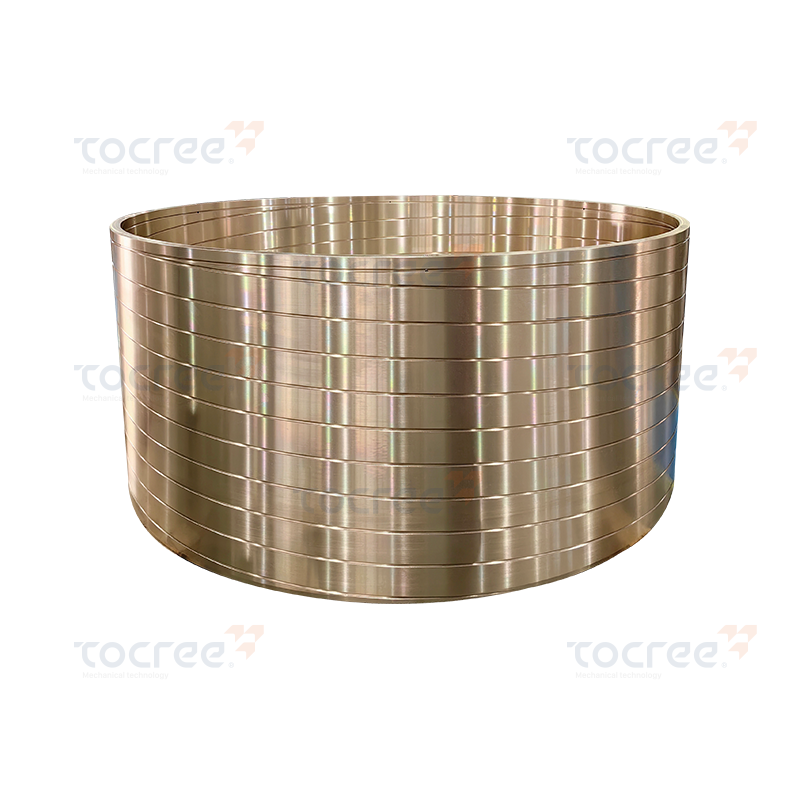 Bronze Bushing
This bronze sleeve is made of tin bronze as the base material. The blank piece is produced...
-
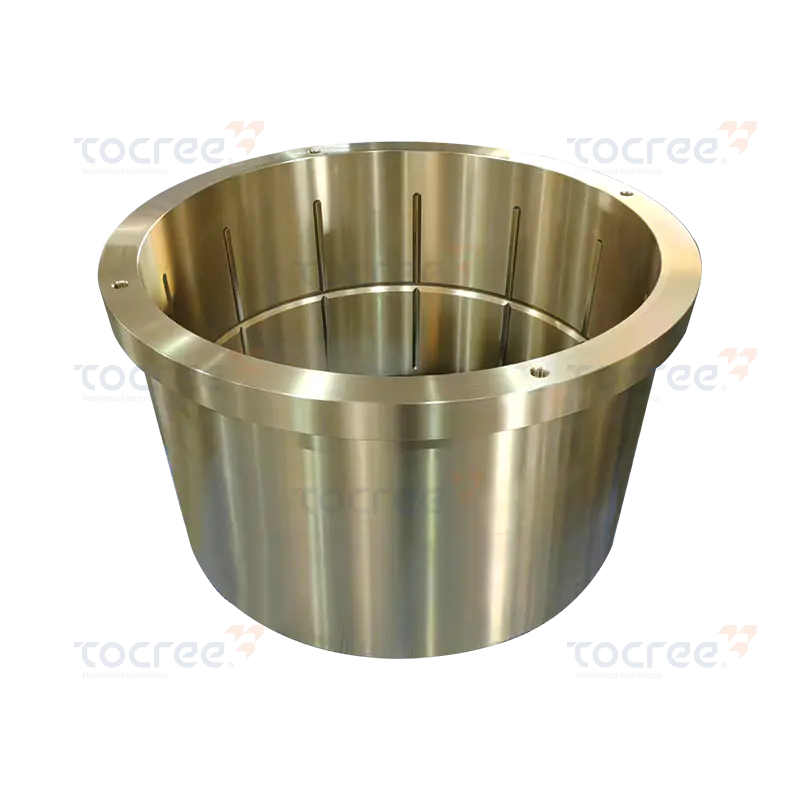 Brass Bushing with Grease Groove
This brass sleeve is made by centrifugal casting with a copper-zinc alloy as the base mate...
-
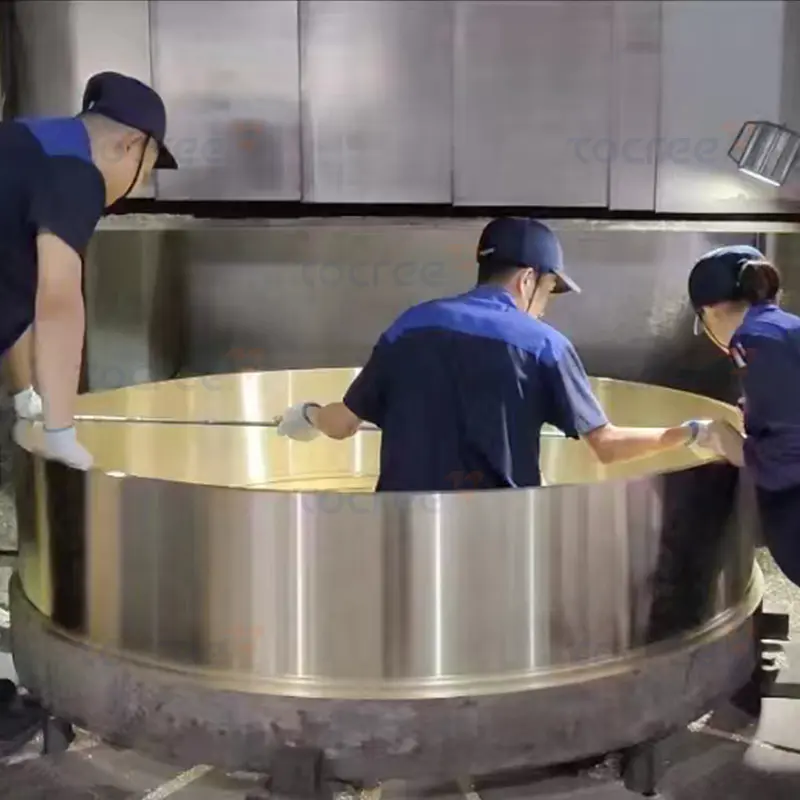 Brass Bushing for Large Industrial Bearing
This high-performance brass single flange sleeve is specially designed for large industria...
-
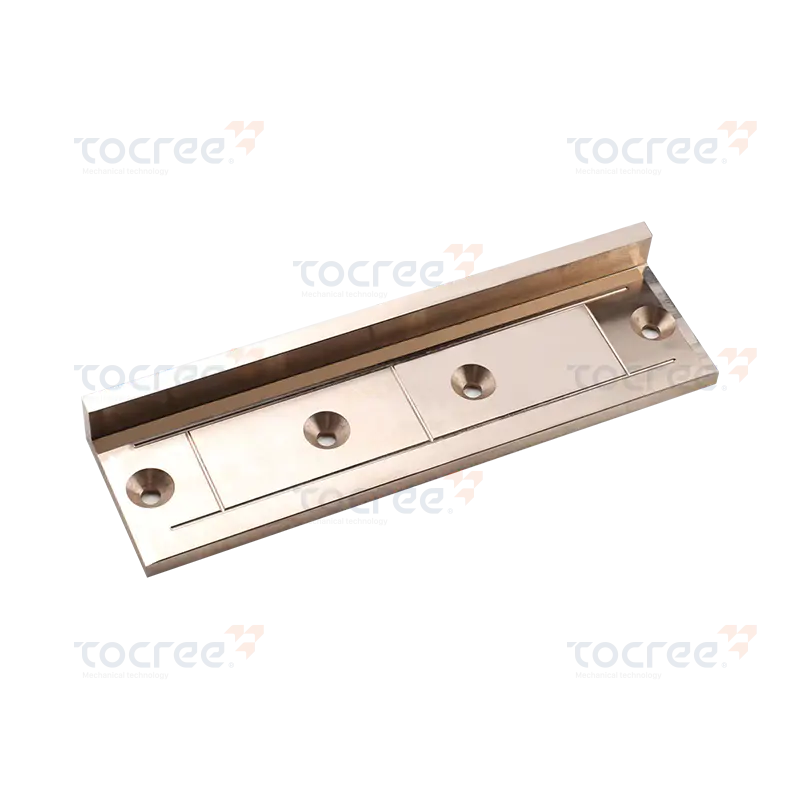
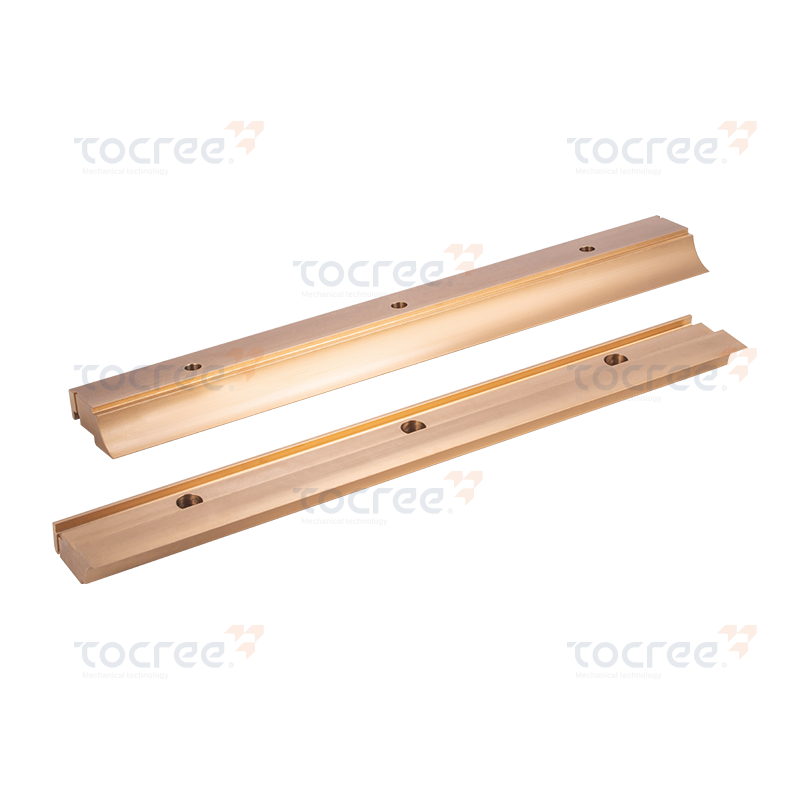 Bronze Linear Slide Block
This linear slide board is a high-performance sliding component, made of excellent tin bro...
-
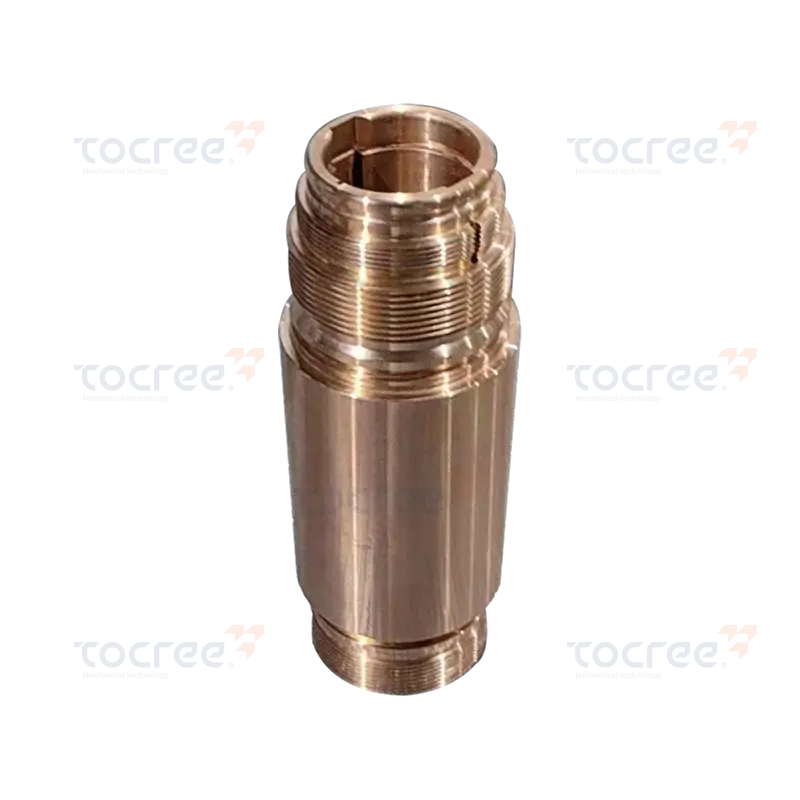 Threaded Copper Bushing
This threaded copper sleeve is a high-performance component. It is made from tin bronze an...
-
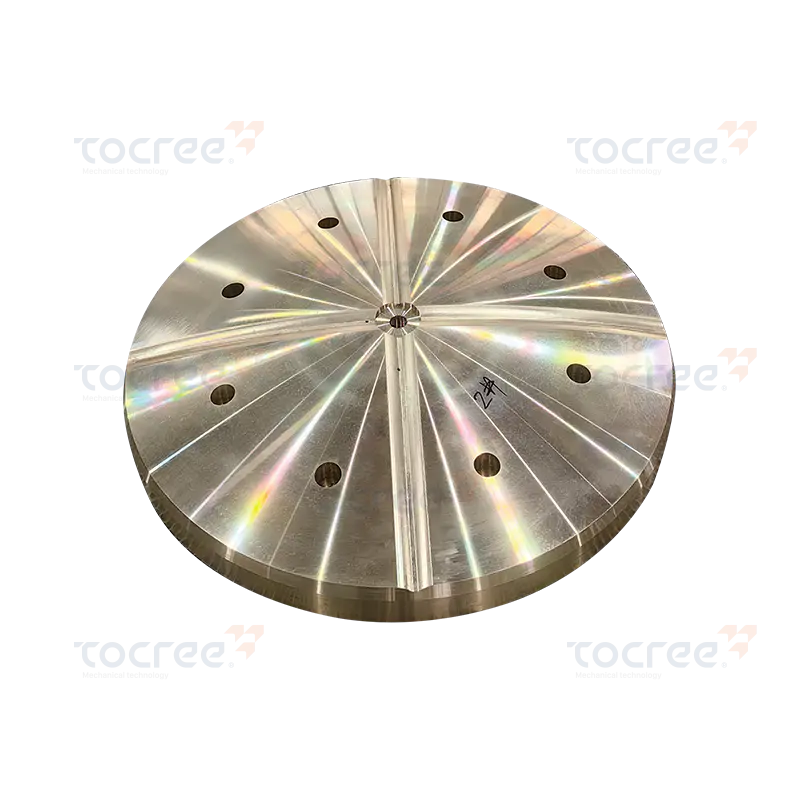 Copper-based Spherical Thrust Washer
The copper-based spherical thrust plate is a high-performance copper alloy component, made...
-
-
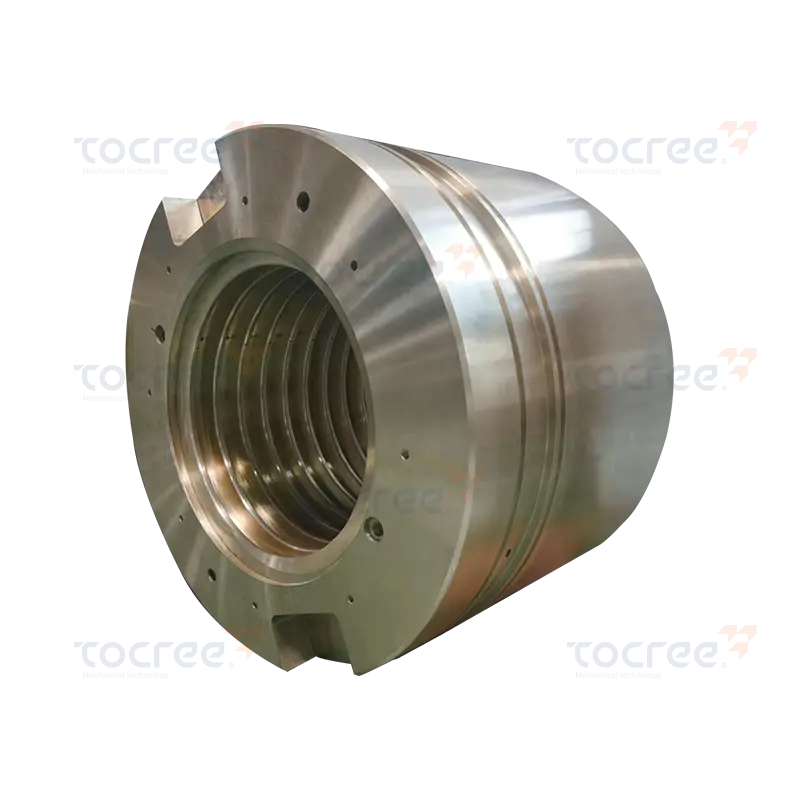 Special-Shaped Copper Nut
This product is a high-quality copper nut, made from tin bronze as the base material throu...
-
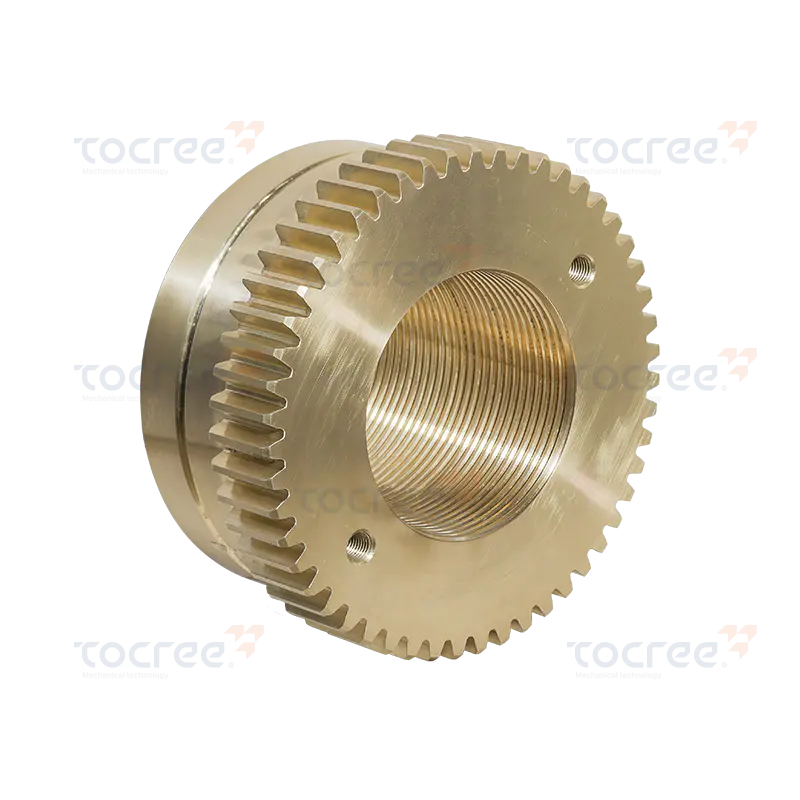 Bronze Hobbed Nut
This copper-based gear nut is a high-performance component. It is precisely machined from ...
WHO ARE WE
A Professional Copper Alloy Casting Company Integrating Casting And Precision Machining
+ contact us
Founded in 2007, Jiashan Tocree Machinery Co., Ltd. covers an area of about 30000 square meters and has a registered capital of 11 million yuan. It is located at No. 18, Zhensheng Road, Weitang Sub-district,Jiashan County Zhejiang Province, China, enjoying a superior geographical location and convenient transportation.
With rich experience in the production and processing of non-standard parts and precision machining, it is a research and development-oriented manufacturing enterprise integrating research and development, sales, design and processing. As Graphite Bronze Bushing Manufacturers and Graphite Bronze Bearing Suppliers in China, The company is well-equipped and has extensive experience, committed to producing finished steel sleeves, copper sleeve plates (including special-shaped parts) and copper products of various sizes, shapes and materials.
It specializes in the production of copper mining machinery parts made of various copper alloys (phosphor bronze, tin bronze, aluminum bronze, beryllium bronze). The products are widely used in metallurgical machinery, ships, mining machinery, engineering machinery, agricultural machinery, large construction machinery, large packaging machinery and mold industries.
We have copper sleeves as large as 1.5-2 meters; copper sliding plates as long as 4 meters, 400mm wide and 100mm thick; and other mechanical copper parts, such as copper nuts, copper gears, copper sleeve worm wheels, rollers and other mechanical accessories. The company is well-equipped, with its own copper smelting furnace and centrifuge, etc. It specializes in the production of copper materials of various types, with an annual output of 2300 tons. It provides copper raw material billets for our company and is a one-stop manufacturer from raw materials to finished products. Provide Bronze Guide Bushing for sale.
The company has a high-quality and strong technical team, sophisticated mechanical processing equipment, and is equipped with precise testing and experimental equipment. For a long time, the company has adhered to the market-oriented business policy, insisting on "providing high-quality services for customers, based on development and innovation, and strengthening is the last word". Guided by market-demanded products, on the road of continuous innovation and progress, good market demand is the foundation of the company's survival. With the company's current advantages, it serves customers' needs and achieves the goal of win-win cooperation and common development.
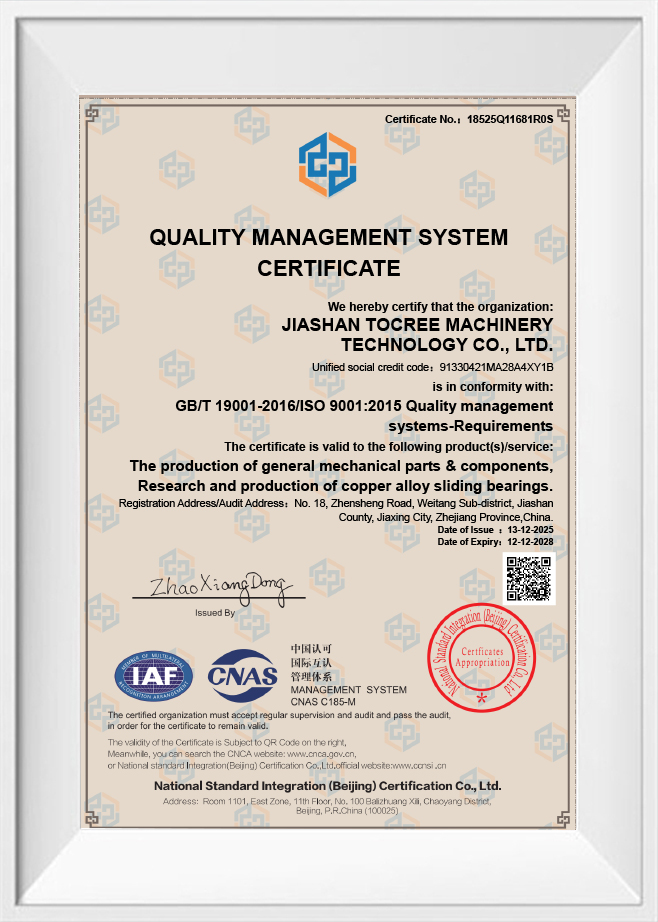
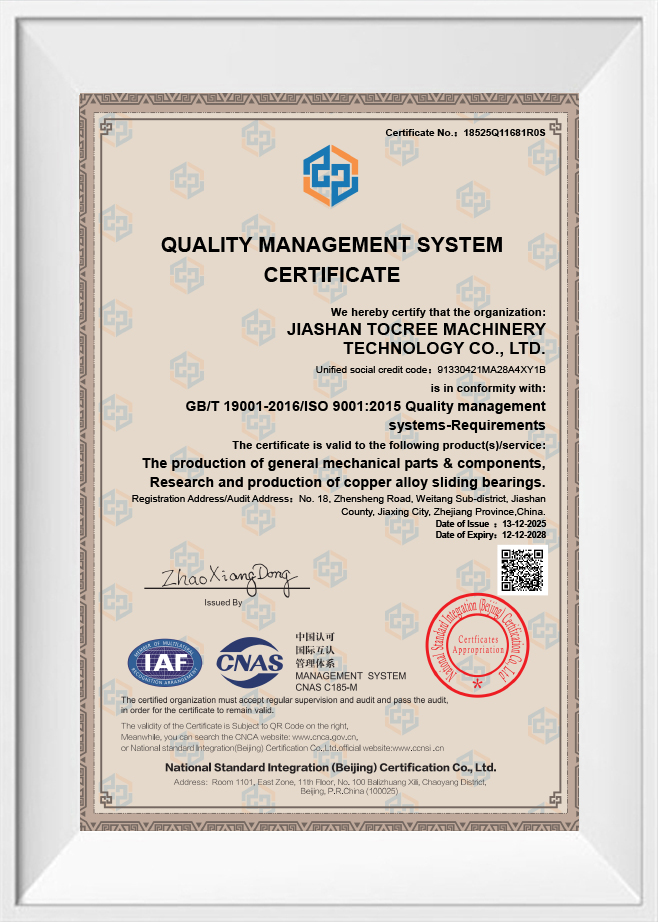
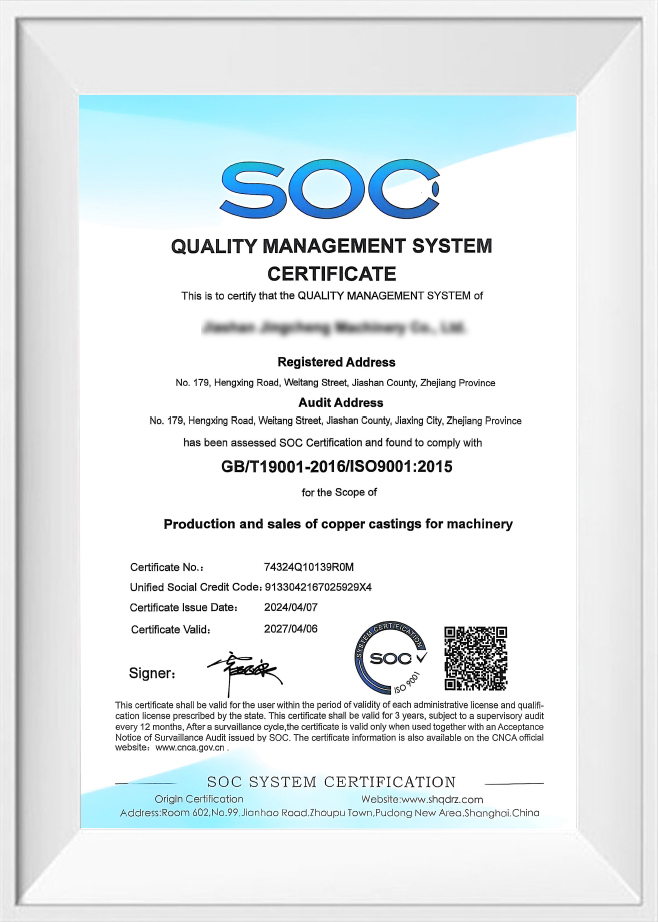
Certificate Of Honor
News
-
Anyone who has crawled under a machine with a grease gun knows the feeling: the fittings sit in the worst possible place, and the maintenance schedule never quite matches producti...
READ MORE -
Anyone who has spent time on a plant floor knows that wear rarely announces itself. It shows up as a machine that slowly stops holding tolerance, a guide that needs shimming every...
READ MORE -
Visit us at Booth AJ34, November 18–21, 2026 Jiashan, Zhejiang, China – October 2026 – Jiashan Tocree Machinery Co., Ltd. (Tocree Machinery) today announced that it will participat...
READ MORE -
Invitation to SHIPTEC China 2026 We are pleased to announce that Jiashan Tocree Machinery Co., Ltd. will exhibit at the 17th International Shipbuilding, Marine Equipment and Offsho...
READ MORE -
A copper alloy curved slider is a small part with a large job. It is the arc-shaped bronze or brass block that rides along a curved guideway, takes the load, and keeps two moving ...
READ MORE
Industry Knowledge
How Graphite Plug Placement Determines Self-Lubrication Performance
In a graphite bronze bushing, the graphite is not simply mixed into the bronze matrix — it is inserted into precisely drilled or cast holes distributed across the bearing's working surface. The pattern, density, and depth of these graphite plugs directly determine how the bushing behaves under load. A denser plug arrangement near the high-pressure zone of the bearing improves lubrication exactly where friction is greatest, while a uniform grid pattern is better suited for bushings that see load from multiple directions, such as swing arms or rotating shafts. As the bronze surface wears during operation, the graphite plugs gradually release a thin lubricating film, which keeps functioning even if external lubrication is interrupted for a period of time. This is why graphite bronze bearings are frequently chosen for equipment where routine greasing is difficult or inconsistent, such as remote mining machinery or large construction equipment operating in dusty environments.
Typical Graphite Coverage Ratios by Application
| Application | Recommended Graphite Coverage | Typical Load Type |
| Excavator swing bearings | 25%-30% | Oscillating, high shock |
| Conveyor rollers | 15%-20% | Continuous, low speed |
| Hydraulic cylinder pins | 30%-35% | High pressure, limited rotation |
Choosing Wall Thickness for Brass Bushings Under Radial Load
A common mistake in specifying brass bushings is treating wall thickness as a fixed ratio of the shaft diameter, when in reality it should be calculated against the expected radial load and the housing's rigidity. A bushing with too thin a wall will deform under sustained radial pressure, losing its interference fit and eventually spinning inside the housing bore. On the other hand, an oversized wall thickness increases material cost and can reduce heat dissipation, since brass relies partly on its own mass to conduct frictional heat away from the contact surface. For medium-duty applications such as agricultural machinery linkages, a wall thickness between 8% and 12% of the shaft diameter is generally sufficient. For heavy construction or metallurgical equipment where shock loading is common, thicker walls in the 12%-18% range provide a better safety margin. We machine each brass sleeve to the customer's actual load specification rather than defaulting to a standard ratio, which avoids both premature wear and unnecessary material waste.
Common Failure Modes in Bronze Sleeve Bearings and Their Root Causes
Understanding why a bronze bushing fails is more useful than simply replacing it, because most failure patterns point back to a specific installation or operating issue that will repeat if left uncorrected. Below are the failure modes most frequently seen in metallurgical and mining machinery applications.
- Scoring or scratching on the inner bore usually indicates contaminated lubricant or abrasive particles entering through a damaged seal, rather than a defect in the bushing material itself.
- Localized wear on one side of the bushing points to shaft misalignment or housing bore distortion, not insufficient hardness of the bronze alloy.
- Cracking near the bushing edges is often caused by excessive press-fit interference during installation, which induces hoop stress that later propagates under cyclic loading.
- Discoloration or bluish tint on the bronze surface signals overheating from inadequate lubrication frequency, which gradually reduces the alloy's fatigue resistance.
- Rapid wear at start-up but stable performance afterward is typical of boundary lubrication conditions, and is common in bushings without embedded graphite where oil film has not yet formed.
Matching Copper Alloys to Working Conditions
Not every copper alloy performs the same way under identical conditions, and choosing the wrong one is a frequent cause of underperformance in heavy machinery. Since we operate our own copper smelting furnace and centrifuge, we control alloy composition from the raw billet stage, which lets us adjust the mix depending on whether a part needs higher load resistance, better corrosion resistance, or lower friction. The table below summarizes how the four alloys we most commonly work with compare against one another.
| Alloy | Load Capacity | Corrosion Resistance | Best Suited For |
| Phosphor Bronze | High | Good | Gears, worm wheels, heavy sliding plates |
| Tin Bronze | Medium-High | Very Good | Marine and shipbuilding components |
| Aluminum Bronze | Very High | Excellent | Mining machinery, high-impact parts |
| Beryllium Bronze | High | Good | Precision molds, spring-loaded components |
Clearance Fit Guidelines for Large-Diameter Copper Sleeves
When a copper sleeve reaches 1.5 to 2 meters in diameter, standard small-part fit charts no longer apply, because thermal expansion, machining tolerance stack-up, and housing distortion all scale differently at that size. For large sleeves, we typically machine a running clearance of 0.001 to 0.0015 times the shaft diameter, adjusted upward slightly if the equipment operates in high-temperature environments such as metallurgical plants, since copper alloys expand more than the steel shafts they pair with. Cutting the clearance too tight on a large sleeve risks seizure once operating temperature rises, while too loose a fit causes vibration and accelerated edge wear. For long copper sliding plates, such as the 4-meter units we produce, flatness tolerance across the full length matters as much as clearance, since even a slight bow will concentrate load unevenly along the plate.
Maintenance Practices That Extend Bushing Service Life
Extending the service life of a bronze bushing usually comes down to a handful of maintenance habits rather than upgrading the material itself. Establishing a lubrication interval based on actual operating hours, rather than a fixed calendar schedule, accounts for variations in load and speed that a calendar cannot. Inspecting the shaft surface finish periodically is equally important, since a roughened or corroded shaft will abrade even a high-quality bushing regardless of alloy choice. For graphite bronze bearings specifically, monitoring the depth of graphite plug wear during scheduled maintenance gives an early indication of remaining service life before failure symptoms appear.
Quick Reference Maintenance Checklist
- Check radial clearance every 500-1000 operating hours on high-load equipment.
- Inspect graphite plug surface for glazing, which reduces lubricant release.
- Verify shaft surface roughness stays within the original design specification.
- Confirm seal integrity to prevent abrasive contamination from entering the bore.
- Record temperature at the bearing housing during peak load cycles to catch early overheating.
Since our production runs from raw copper billet through to the finished, machined part within a single facility, we're able to adjust alloy composition and graphite plug pattern to match a customer's specific operating conditions rather than supplying a generic off-the-shelf part.
Copyright © 2025 Jiashan Tocree Machinery Co., Ltd. All Rights Reserved.
Graphite Bronze Bearing Suppliers
